How to Read a Golf Bag Tech Pack and Specification Sheet
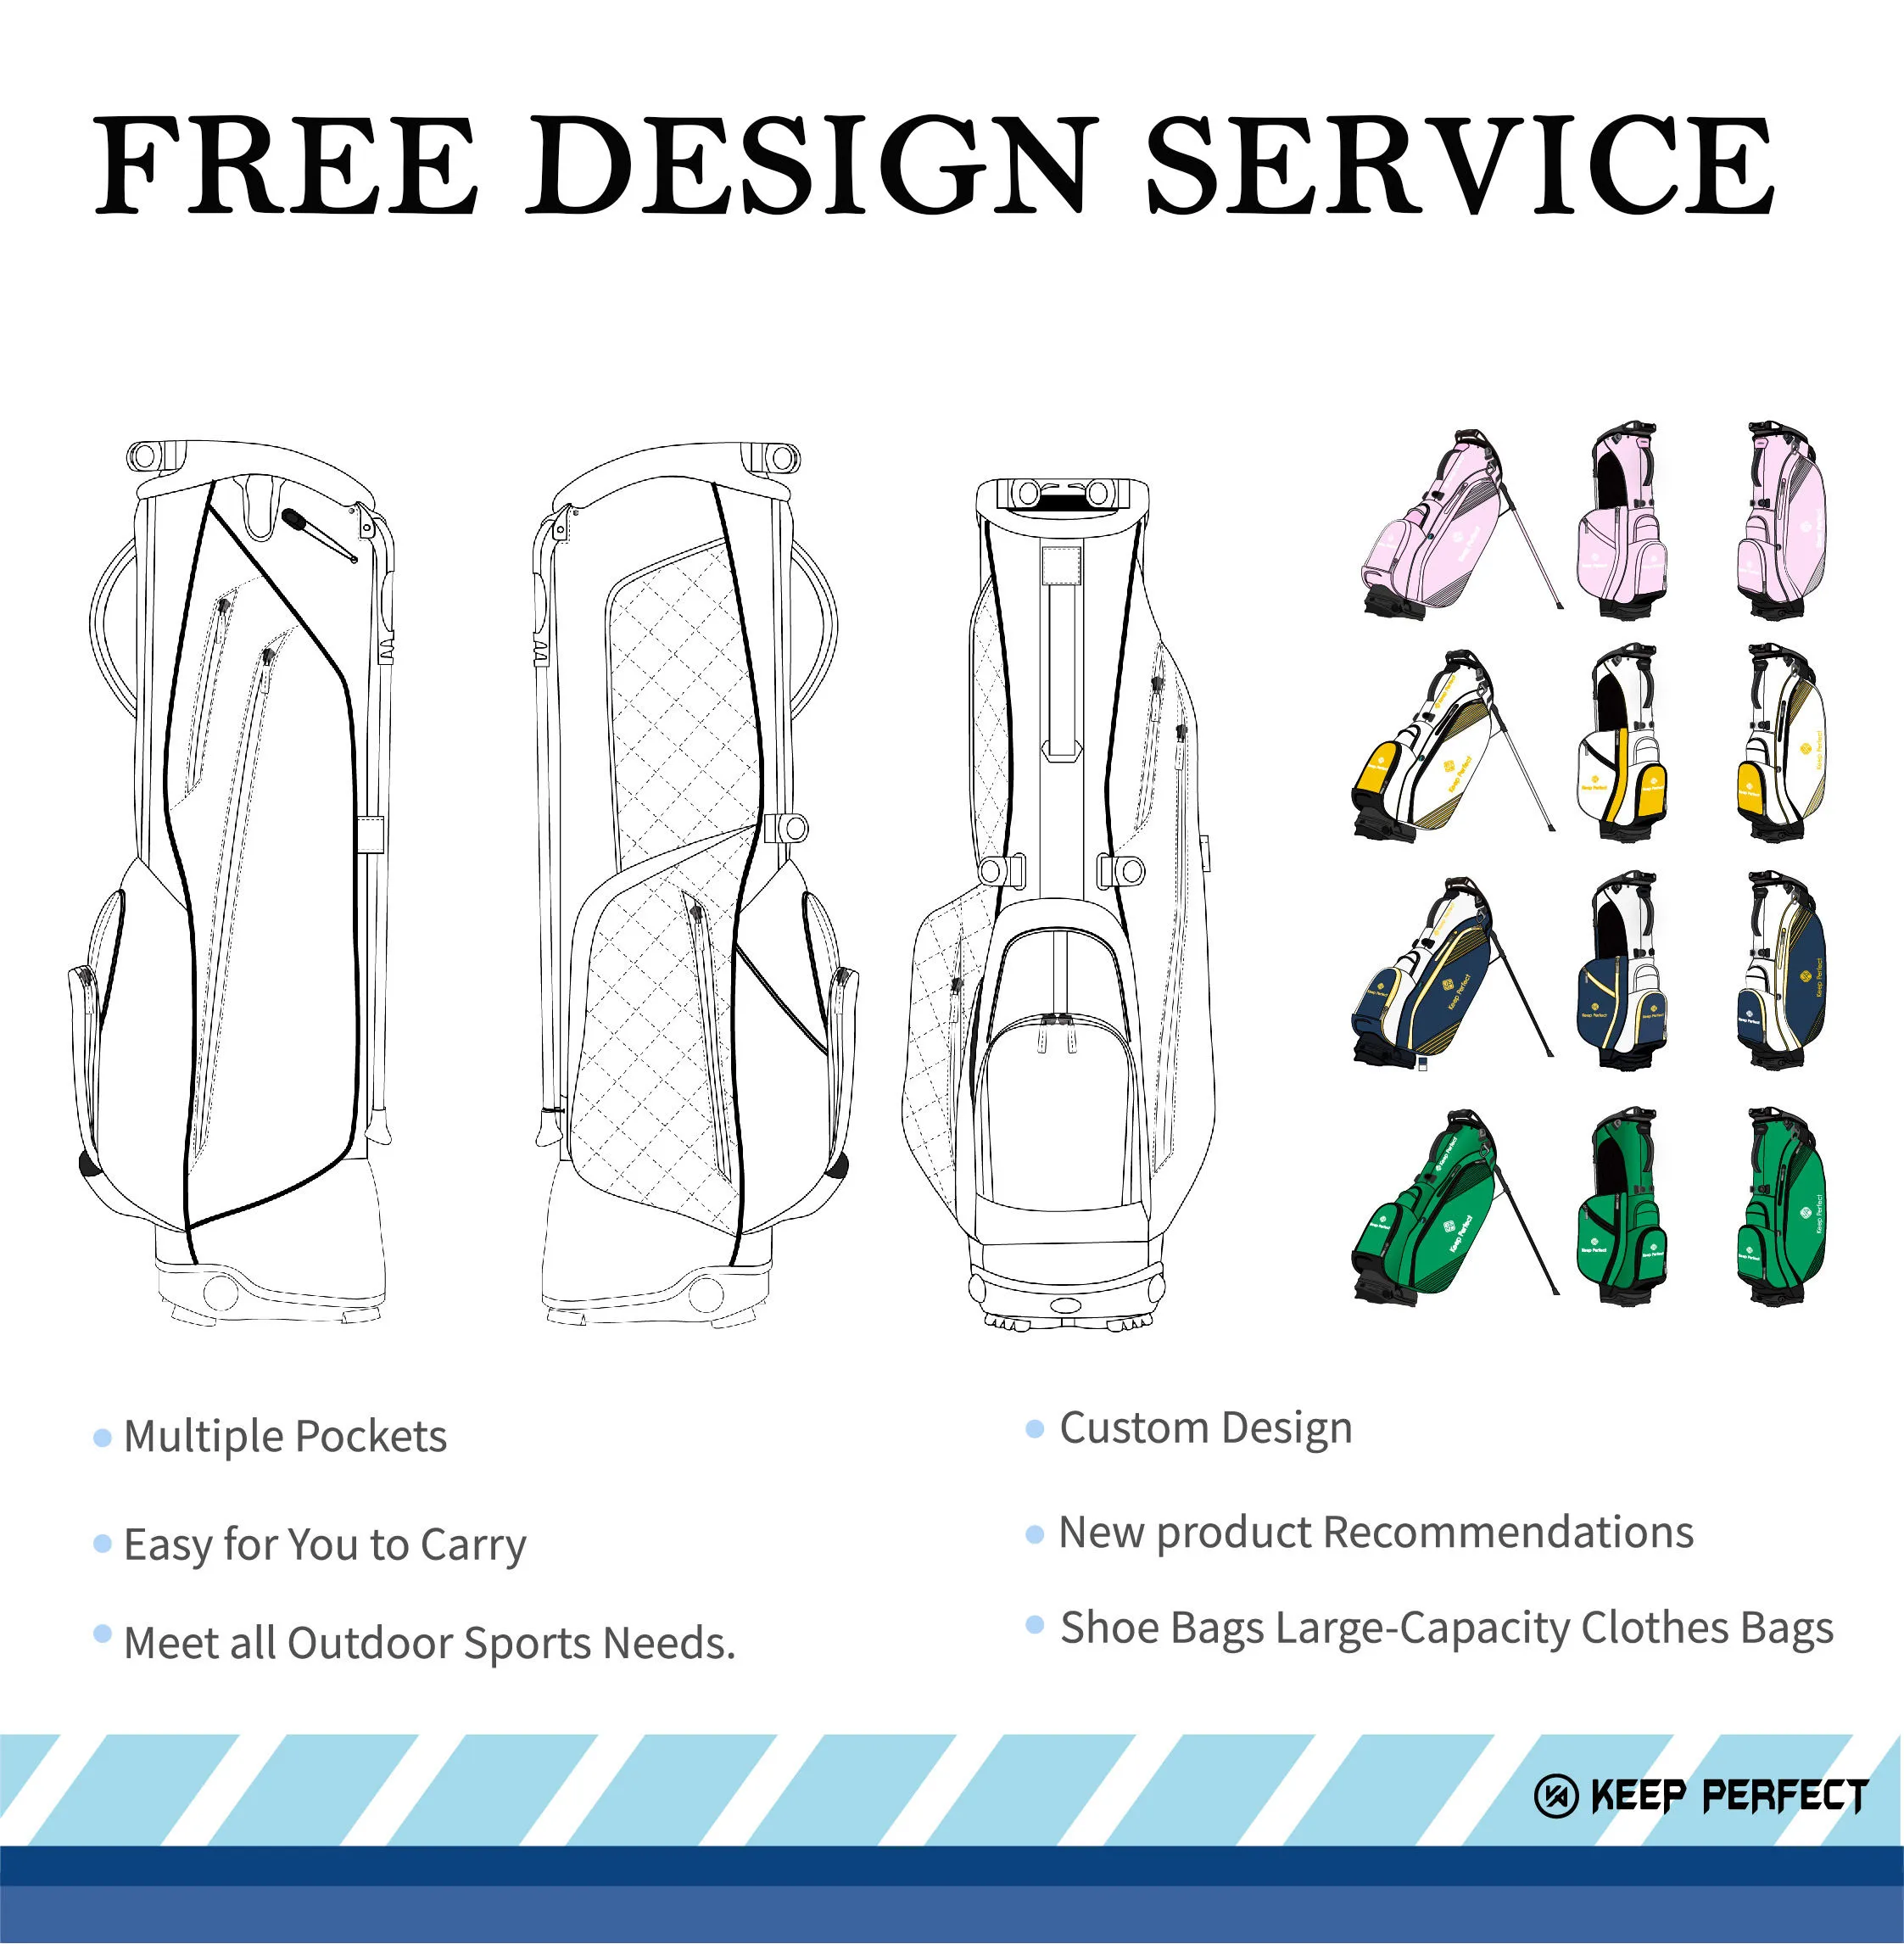
A golf bag tech pack is a set of manufacturing instructions, not a design brief, and every number in it has to be measurable by someone standing at the end of a sewing line. A pack written as mood, material references and a rendered image will produce a beautiful sample and an inconsistent bulk run. A pack written as a bill of materials, a measurement chart with tolerances, construction callouts and an artwork placement page will produce a bag that matches its drawing on unit 20 as well as unit 2. This is a page-by-page read of a well-built pack, with the tolerance values, stitch densities and code conventions that make each page enforceable at inspection.
Related reading: Golf Bag Sample Approval and Color Difference Tolerance
What Belongs in a Tech Pack and What Does Not
A tech pack has one job: to remove ambiguity from a product that is assembled by people who will never meet the designer. Anything that serves that job belongs in the pack. Anything that does not belongs in a separate document, because a pack with padding is a pack that gets skimmed.
Six sections, no padding
The core is six sections: a cover page with style identity and revision control, a bill of materials, construction callouts, a measurement chart with points of measure and tolerances, artwork pages, and packing instructions. Everything else is optional and usually harmful: brand storytelling, retail price positioning, competitor references and mood boards all dilute the instructions that matter. If a supplier has to guess which page governs a decision, the pack has failed.
The single most useful discipline is to write every requirement as a value plus a method plus an acceptance criterion. "Reinforce the strap anchor" is not a requirement, because nobody can fail it. "Bar-tack, 24 mm long, T-90 bonded nylon, 10 stitches per inch, at both ends of each strap anchor, no more than 2 mm from the seam line" is a requirement that an inspector can reject against.
A pack also needs a revision field on every page, not only on the cover. Technical packs change, and the change is almost always local: a pocket height moves, a zip length changes, a logo shifts 3 mm. If the revision number sits only on page one, a supplier printing pages individually can work from a stale page four for a week without noticing.
Page One: Style Number, Colourway and Revision Control
The cover page is admin, and it is where expensive mistakes start. Six fields do the work: style number, style name, colourway code, season or programme, revision number with date, and the name of the person with authority to approve. Without a colourway code, two colour programs share a BOM and the mill ships the wrong trim. Without an approver name, a verbal yes from an account manager becomes an instruction.
The colourway code is worth a paragraph of its own. A three-colour programme should carry three codes, each tied to a lab dip reference and a thread card. Trim colours drift between lots far more than shell colours do, because piping, webbing and binding come from different suppliers. If the code does not travel with the order into the cutting ticket, the sewing line will match trim to whatever is on the shelf.
Revision control needs a simple convention: a two-digit number plus the date, and a one-line change note. Revision 03, 12 August, side pocket height increased from 210 mm to 225 mm. That note is what lets a supplier confirm that the pack it received is the pack that the buyer believes was sent, and it is the first thing to check in any dispute after a bulk run.
The cover should also state the inspection basis, because the rest of the pack assumes it. On our programmes that means sampling to ISO 2859-1 at general level II with an AQL of 2.5, so a 200-piece lot yields 32 units and tolerates two defective bags before the lot is refused. If the buyer wants a different level or a zero-critical rule, this is the page that says so.
The Bill of Materials Line by Line
The BOM is a table of every component with a code, a description, a colour, a consumption figure and a supplier or approval status. It is the page buyers read least carefully and suppliers use most. A BOM that says "600D polyester, black" is not a specification; it is a category.
A usable BOM line reads like this: shell, 600D polyester, 64T construction, PU coated 1,000 mm, WR finish, 168 gsm, black 19-4005, 1.62 m per unit, mill-approved to lab dip L-228. Every element in that line answers a question that would otherwise be asked after the fabric has been cut. The denier sets the yarn; the construction tells the mill whether it is a plain weave or a basket; the coating sets the water resistance; the weight sets the hand; the consumption sets the fabric order.
| BOM element | What it controls | What to confirm in writing |
|---|---|---|
| Denier, e.g. 600D | Yarn weight per 9,000 m, hence body and tear strength | Filament or spun, and whether it is a 64T or 68T weave |
| Coating, e.g. PU 1,000 mm | Hydrostatic resistance in millimetres of water | Coated or laminated, and whether seams are taped |
| Finish, e.g. WR | Surface water repellency | Durable to how many washes, and at what spray rating |
| Thread, e.g. T-90 bonded nylon | Seam strength and UV life | Ticket size, bonding, and colour-matched to which reference |
| Zip, e.g. #10 coil | Load capacity on the main opening | Slider brand, metal or nylon, and puller style |
| Consumption, e.g. 1.62 m | Fabric purchasing and cutting spread | Whether it includes wastage and the cut allowance |
Two conventions cause most BOM disputes. The first is consumption: a figure quoted without a wastage allowance produces a fabric order 8-12 per cent short once the cutting spread is laid. The second is the approval status column. A line marked "pending" means the component cannot be ordered, and a pack issued with three pending lines is not ready to sample, however complete the rest of it looks.
The BOM test. Hand the BOM to a mill and ask them to quote from it without further questions. If they come back with questions, the BOM is incomplete, and every question they ask is a question the sewing line will ask later with fabric already cut.
Construction Callouts: Seams, Stitch and Reinforcement
Construction callouts are the pages that separate a bag that survives a season from one that does not, and they are the pages most often written in prose. Prose cannot be inspected. A callout should be a drawn section, a stitch specification and a reinforcement instruction, tied to a named seam.
The values that matter are few and specific. Main structural seams run 7-9 stitches per inch in T-70 or T-90 bonded nylon, with a double-row lockstitch on any seam that carries load, such as the top-to-body join, the base-to-body join and the strap anchors. Bar-tacks go at every anchor point at 8-10 stitches per inch, 20-24 mm long. Binding is 20-25 mm finished width, folded and double-stitched, with the seam allowance graded so the binding does not pull the panel.
Reinforcement is where a pack earns its keep. A golf bag fails at four places: the strap anchors, the base-to-body join, the top collar junction and the pocket corners. Each needs a named reinforcement: a webbing patch or a box-X at the anchors, a double-stitched and taped base join, a bar-tack at the collar junction, and a triangular or rounded reinforcement at the pocket corners rather than a square one, because a square corner concentrates stress.
Callouts should also cover the parts nobody photographs. Zip ends need a fabric garage or a storm flap on the two openings that face the weather. The cart strap channel needs to be as wide as the widest cart strap the target market uses, and it needs a reinforcement behind it or the shell abrades through in a season. The umbrella sleeve needs a drain hole and a base that does not collect water. A pack that specifies these is a pack written by someone who has seen returns.
One practical convention: number every callout and place the number on both the drawing and the construction page. When a first article arrives with a 6 mm binding instead of 20 mm, the conversation is about callout 12, not about a general impression that the trim looks thin.
The Measurement Chart: Points of Measure and Tolerance
The measurement chart is the most argued-over page in any pack, because it is the page an inspector measures against. It has three columns that must all be filled: the point of measure, the target value with a tolerance, and the method. A target without a tolerance cannot be inspected; a tolerance without a method cannot be agreed.
| Point of measure | How it is measured | Target and tolerance |
|---|---|---|
| Overall height | Base seam to top rim, bag upright, empty | 910 mm, plus or minus 10 mm |
| Top oval, width and depth | Inside the collar, both axes, empty | 255 x 200 mm, plus or minus 3 mm |
| Body width at base | Flat, across the widest point, no tension | 330 mm, plus or minus 5 mm |
| Side pocket height | Top edge of pocket opening to pocket bottom seam | 225 mm, plus or minus 3 mm |
| Divider wall height | Top rim to lowest point of the wall | 60 mm, plus or minus 3 mm |
| Strap length, centre to centre | Anchor to anchor, laid flat, no load | 1,050 mm, plus or minus 10 mm |
| Logo placement | Centre of mark to nearest seam, both axes | Plus or minus 2 mm |
| Finished weight, empty | Calibrated scale, bag only, no packaging | 2.35 kg, plus or minus 50 g |
Three rules make the chart work. Measure the assembled bag, not the cut panel, because lining and lamination add 1.5-3 mm in every direction. State the condition: empty, upright, no load, at 20 degrees Celsius. And measure to the nearest millimetre with a steel rule, not a tape, because a tape sags over 900 mm and introduces 3-5 mm of error that then gets argued about as a defect.
The tolerance values themselves should be chosen by function rather than by habit. A top oval at plus or minus 3 mm is tight because it has to sit in a cart cradle and hold the divider. A pocket height at plus or minus 3 mm is generous, because nothing depends on it. A strap length at plus or minus 10 mm is generous on paper and tight in practice, because a strap that is 20 mm short changes where the bag sits on the shoulder.
Tolerance stacking is the reason a pack cannot be written point by point in isolation. The top oval feeds the collar, the collar feeds the divider, and the divider feeds the body height. A 3 mm error at the top can become a 7 mm error at the base after assembly, which is why the chart should carry a note on which dimensions are critical and which are reference.
Weight is a measurement too. A finished-weight figure with a 50 g tolerance catches more problems than three dimensional checks, because it flags a substituted fabric, a missing reinforcement or an extra layer of padding in one number. Weigh every first article and every pre-production sample.
Artwork Pages: Placement, Size and Colour Match
The artwork page does three jobs: it fixes the geometry of every mark, it defines the colour, and it states the process. Geometry means position, size, orientation and which panel. Colour means a Pantone reference for print, a thread code for embroidery and a ΔE limit for anything that has to match the shell. Process means screen print, embroidery, heat transfer, emboss or a woven label, because the same artwork behaves differently in each.
Dimension from a seam, not from a photograph
Placement should be dimensioned from a seam, not from the edge of a photograph. "Logo centred on the front panel, 40 mm below the top rim seam" is checkable. "Logo on the front" is not. For a mark that appears on a curved panel, add a note on how the artwork is to be distorted for the curve, because a flat transfer applied to a compound curve will pucker at the corners.
Colour tolerance for a printed mark is normally ΔE 1.5 or better against the approved standard, measured under D65. For embroidery, the limit is a thread card match, and the practical risk is a dye lot difference in the thread rather than a measurement error. For a mark that has to sit on a black shell, the more useful specification is the contrast requirement plus the ink opacity, because a thin white print on 1680D will show the weave regardless of how well the colour matches.
The last artwork field buyers forget is the approved sample reference. Every artwork page should name the physical standard: a signed strike-off, a sewn-off on the actual shell fabric, a printed plaque. Digital references drift because screens differ. A sewn-off on the production fabric, kept as the master, ends the argument before it starts.
Packing, Carton and Labelling Instructions
Packing is the least glamorous page and the one that decides whether a container load arrives saleable. It should state the poly bag or dust bag specification, whether the bag is stuffed or flat-packed, the carton dimensions and unit count, the carton grade, the marking layout and the label content.
Carton counts decide the container plan
Carton counts for golf bags land between 4 and 10 units depending on type: a staff bag is bulkier and packs 4-6, a cart bag 6-8, a stand bag 8-10. The number matters commercially because it changes the container plan, and it matters physically because a carton rated for 8 bags will crush if the loading team stacks it ten high. State the maximum stack height and the compression strength in the same page.
Labels should carry the style number, colourway code, size or type, carton number and total, and the country of origin marking required at destination. If the buyer is shipping to a retail distribution centre, add the barcode format and placement, because a carton that arrives without a scannable label is either reworked at the DC or refused.
The page should also cover what goes inside the bag: hangtags, silica, warranty cards, and any insert. These items are cheap and they are the most common cause of a short shipment, because they are packed at the end of the line by someone working from memory. If the pack does not list them, they will not be there.
A Reading Order for a Pack You Have Just Received
A pack that arrives from a brand, an agency or a previous supplier should be read in a fixed order, because reading the measurement chart before the BOM produces a sample built from the wrong cloth. The sequence below takes 40-60 minutes and finds the problems that would otherwise surface at first article.
- Cover page first. Confirm the style number, the colourway code and the revision date against the email that carried the pack. If the revision does not match, stop and ask which version governs.
- Count the colourways against the BOM. Every colourway needs its own trim, thread and lab dip reference. A three-colour programme with one BOM line is a pack that will produce three inconsistent bags.
- Read the BOM for pending status. Any component not approved cannot be ordered. Flag those before anything else, because they set the sampling date.
- Check consumption figures for a wastage allowance. A number quoted per unit without 8-12 per cent wastage will under-order fabric and force a substitute on the second cut.
- Read every callout for a stitch count and a thread size. Where the page says only "reinforce", write the missing value yourself and send it back for confirmation.
- Read the measurement chart for method and tolerance. Mark which dimensions are critical to function and which are reference, and query any target with no tolerance.
- Read the artwork pages against the physical standard. If the only reference is a digital file, request a sewn-off or a printed strike-off before sampling starts.
- Read packing last and separately. It does not affect the sample, but it affects the freight quote, the carton plan and whether the goods are accepted at the destination.
Whoever reads in this order will usually send back between six and fifteen queries. That is not a sign of a bad pack; it is the normal condition of a document written by one team and executed by another. The failure mode is a pack that generates no queries at all, because it means nobody has read it closely enough to notice what is missing.
Red Flags That Cost You a First Article
Most disappointing first articles are predictable from the pack alone. Six signals account for the majority, and each one is visible before a sample is cut.
- A dimensional target with no tolerance. The supplier will aim for the target exactly, which is impossible, and the sample will be judged against an unstated expectation.
- A BOM with pending components. Anything not approved cannot be ordered, so the sample is built from a substitute and the comparison is meaningless.
- Construction described in prose only. No stitch count, no thread size, no reinforcement position means no way to hold the seam to a standard.
- Artwork with no physical standard. A digital logo file will be interpreted, and the interpretation will be different on the second order.
- Pages without individual revision numbers. A stale page four is the most common source of a wrong pocket height on a repeat run.
- No stated inspection basis. Without an AQL level and a defect classification, the pass or fail conversation happens at the end, when nothing can be changed cheaply.
The remedy is a read-back, not a rewrite. Before a pack is released, the supplier should return a one-page list of every value it cannot meet, every component it cannot source and every method it intends to change. That list takes an hour to produce and typically removes one full sampling cycle, which at 6-10 working days per cycle is the cheapest time a buyer will ever save.
For the sequence that follows a pack, the sampling stage page shows how the first article is produced and measured, and the materials guide expands the BOM codes covered here. Buyers working on a first style often find the customisation process walkthrough a useful companion, because it maps each pack section to the point in production where it gets tested.
Sources and Standards Referenced
- ISO 2859-1:2022 Sampling procedures for inspection by attributes
- ASTM D5034 Breaking strength and elongation of textile fabrics (grab test)
- ASTM D2261 Tearing strength of fabrics (tongue method)
- ISO 105 colour fastness test series, textiles
- ISO TC 38 textiles standards index
Next steps: custom solutions, manufacturing capability, and a quotation request.
Frequently Asked Questions
What is a golf bag tech pack?
It is the manufacturing instruction set for one style: cover page with revision control, bill of materials, construction callouts, a measurement chart with points of measure and tolerances, artwork pages and packing instructions. It is written to be measured against on a sewing line, not to present a design idea.
What tolerance should a golf bag measurement chart use?
Choose by function. A top oval at plus or minus 3 mm, an overall height at plus or minus 10 mm, a pocket height at plus or minus 3 mm, a strap length at plus or minus 10 mm and a logo position at plus or minus 2 mm cover most cart and stand bags. State the measuring condition on every line.
How should dimensions be measured on a golf bag?
Measure the assembled bag, empty, upright, at room temperature, with a steel rule rather than a tape. Lining and lamination add 1.5-3 mm in every direction, so a cut panel dimension is not the finished dimension. Measure to the nearest millimetre and record the condition.
What does 600D mean on a BOM?
Six hundred denier, the weight of the yarn per 9,000 metres. It indicates body and tear strength but says nothing about weave, coating or finish, which is why a BOM line also has to state construction, coating in millimetres of hydrostatic head, finish, weight per square metre and the approved lab dip.
What stitch density belongs in a construction callout?
Seven to nine stitches per inch in T-70 or T-90 bonded nylon for main structural seams, with double-row lockstitch on load-bearing joins. Bar-tacks at anchor points run 8-10 stitches per inch at 20-24 mm long. Without a number the seam cannot be inspected.
Where do golf bags fail most often?
Strap anchors, the base-to-body join, the top collar junction and pocket corners. Each needs a named reinforcement in the pack: a webbing patch or box-X at the anchors, a double-stitched and taped base join, a bar-tack at the collar and a rounded or triangular pocket corner.
Why does revision control matter on every page?
Because changes are local. A pocket height or a logo position moves and the rest of the pack does not change. If the revision number is only on the cover, a supplier printing pages individually can work from a stale page for a week. Put the number and date on every page.
What is a points of measure chart?
A table listing each measured dimension, the method used to measure it and the target with a tolerance. It is the page an inspector works from, so it needs all three columns. A target without a tolerance cannot fail, and a tolerance without a method cannot be agreed.
How do I specify logo placement precisely?
Dimension from a seam, not from a photograph. State the panel, the distance from a named seam on both axes, the size, the orientation and the process. For curved panels, add a note on distortion. Keep a sewn-off on the production fabric as the physical standard.
What should a packing page include?
Poly bag or dust bag specification, stuffed or flat pack, carton dimensions and unit count, carton grade and maximum stack height, marking layout, label content, barcode format and every insert that goes inside the bag. Inserts are the most common cause of a short shipment.
How many bags fit in a carton?
Usually 8-10 stand bags, 6-8 cart bags and 4-6 staff bags, depending on size and stuffing. The figure changes the container plan and it changes the carton strength required, so state the maximum stack height alongside the unit count.
What is the fastest way to improve a weak tech pack?
Ask the supplier for a read-back: a one-page list of every value it cannot meet, every component it cannot source and every method it intends to change. That list typically saves one sampling cycle, and a cycle costs 6-10 working days, or 12-15 where new tooling is involved.
Send Your Tech Pack for Review
Upload the pack as it stands and you will get a marked-up read-back within two working days listing the missing tolerances, pending components and unmeasurable callouts.
Request a Pack Review See Sampling